Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Address
304 North Cardinal
St. Dorchester Center, MA 02124
Work Hours
Monday to Friday: 7AM - 7PM
Weekend: 10AM - 5PM
Plan an aluminum extrusion motor casing with profile DFM, alloy selection, machining stock, cooling features, finish and production inspection.
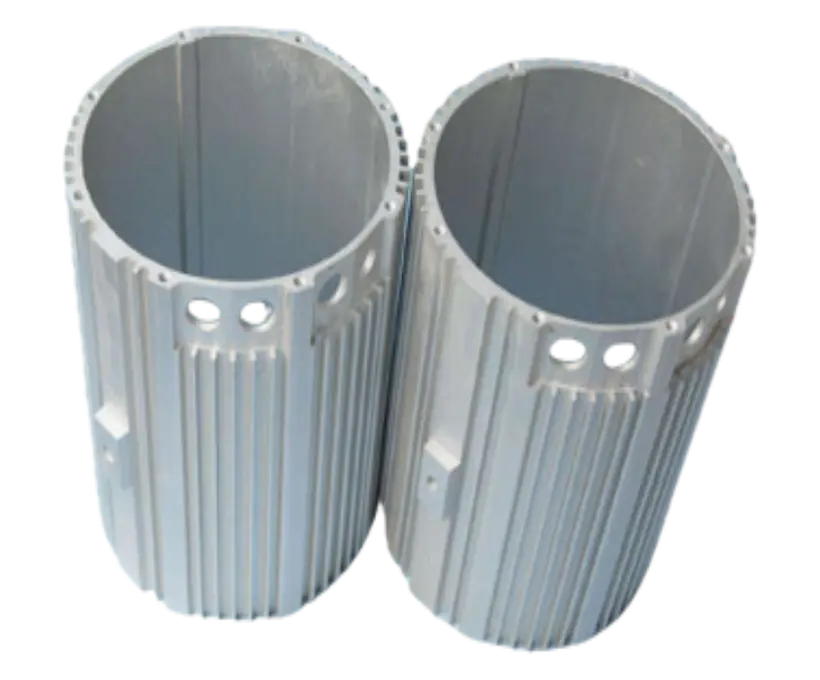
Aluminum Extrusion Motor Casing is best evaluated as a complete engineering and production decision. An aluminum extrusion motor casing is produced around a repeatable cross-section and machined into the finished housing. The most effective route combines extrusion, machining and finishing decisions before tooling begins.
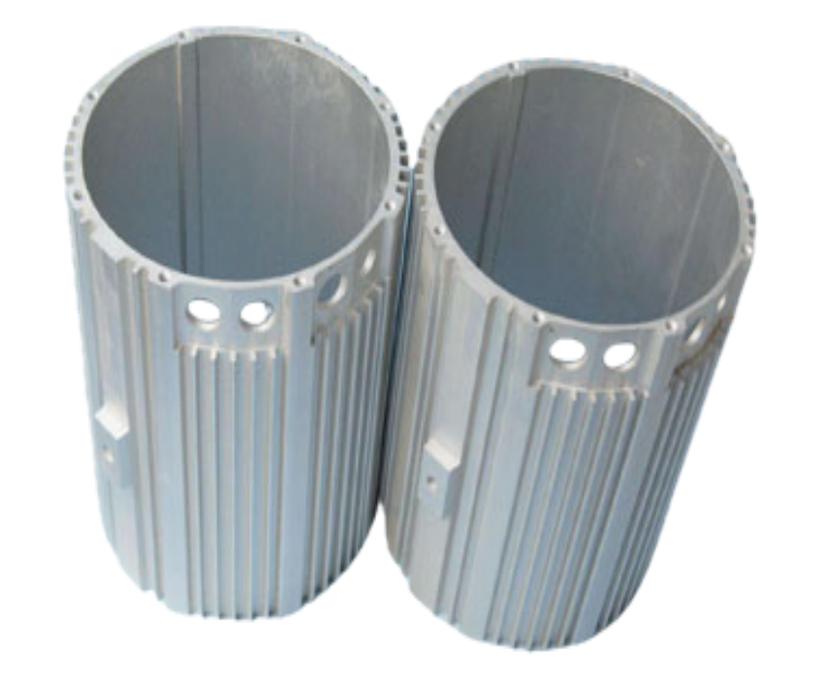
Motor casings often require an internal bore, mounting faces, cooling fins, cable openings and end-cap interfaces. Each feature should be placed where extrusion and machining can produce it consistently. The objective is not simply to select aluminum; it is to define a repeatable component that meets fit, thermal, electrical, corrosion and assembly requirements.
Use the following points to turn the application target into a manufacturable specification:
In addition, confirm the critical dimensions with the team responsible for tooling, machining and inspection. For example, a tolerance that works on a drawing may be impractical if the datum cannot be reached during machining.
The manufacturing route should be reviewed before the die, fixture or finish is committed. A practical sequence is:
Therefore, keep the drawing, sample approval, process specification and inspection plan aligned. If one changes, check whether the others still reflect the finished component.
Inspection should focus on the characteristics that control fit and function. The exact sampling plan belongs in the approved drawing and purchase specification.
Supplier evaluation should go beyond the lowest per-kilogram price. Ask how the supplier will control the die, incoming alloy, wall thickness, straightness, machining datums and finish. In addition, confirm what is measured on the first article and what is checked during repeat production. A lower quote can become expensive if it adds sorting, rework or assembly delays.
Compare the complete production route, including tooling, samples, machining, finishing, inspection, packaging and freight. Therefore, request a quotation that separates these items and states the assumptions. This makes it easier to compare suppliers fairly and to see which design changes will reduce total cost.
Before approving production, connect the supplier’s process plan with your own assembly requirements. For example, identify the surfaces that set alignment, the threads that carry load and the finish areas that must remain free from damage. Clear acceptance criteria reduce disputes and make repeat orders more predictable.
HIQ supports motor housing profiles for servo, gear, traction and industrial drive applications. See the wider motor housing collection for standard sections and custom routes.
Where material standards need clarification, the Aluminum Association and ASTM International publish useful references. Final acceptance criteria should still follow the approved drawing and project specification.
For a related production route, review motor casing profiles or HIQ aluminum product families. You can also send the drawing to the engineering team.
A standard profile can be evaluated first, but critical bore and end-cap dimensions may still require custom extrusion or machining.
6063 is common for extrusion and finish quality, while 6061 or 6082 may be considered when higher strength is required.
It depends on straightness, bore tolerance and fixture strategy. Excessive stock adds cost and removes the benefit of extrusion.
